Company
Snack Food manufacturer from the USA.
Application
A large Snack Food manufacturer had a production “bottle-neck” with their Chain-Swivel bucket “Z” neck conveyor delivery system.
Challenge
Product Wastage
- Because of the un-even engagement of the swivel buckets during their incline travel, the product would fall out or miss the bucket causing 300-400 pounds of food to accumulate on the floor around the conveyor during an 8-hour shift. Workers had to gather the products that fell from the buckets = 2 Hours each day.
High maintenance costs
- Wash downtimes between product change-out = 8 Hours
- Weekly Saturday/Sunday preventive maintenance (Chain Lube/Bucket reinforce/replace/track wear) = 4 Hours
Safety concerns
- Buckets dislodge from the chain holder and fall creating a “Hard hat” safety area.
- Loud movement noise levels.
Solution:
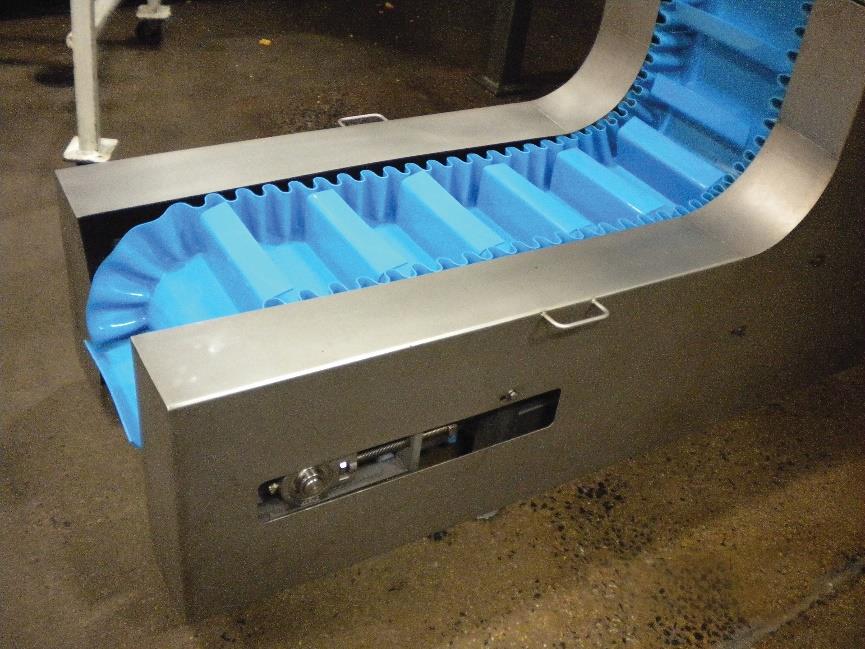
Volta Homogenous Positive Drive Belt with Scoop Cleats & Corrugated Sidewalls
Result
Savings
- Product waste was reduced by 97%.
- Electrical AMP draw was reduced by using a 1.5HP drive motor instead 4HP motor
Maintenance costs
- Daily cleanup of spilled product was reduced from 2 hours to 15 minutes
- Wash downtime between product change-out was reduced from 8 hours to 1 hour
- • Weekly preventative maintenance eliminated. Currently inspected every 6 months without issue
Safety Concerns
- “Hard hat area” eliminated
- Low to little movement noise
Clients` testimonials
Project Engineer stated that: